Comments Off on Press brake crowning: maintaining consistent angles along long bends
Long bends reveal differences that a short sample may hide. Under forming load, the machine and tooling deflect. Crowning compensates for this effect to help achieve a consistent bend angle.. Read More
Comments Off on Press brake tonnage and V-die selection: assess the whole bend
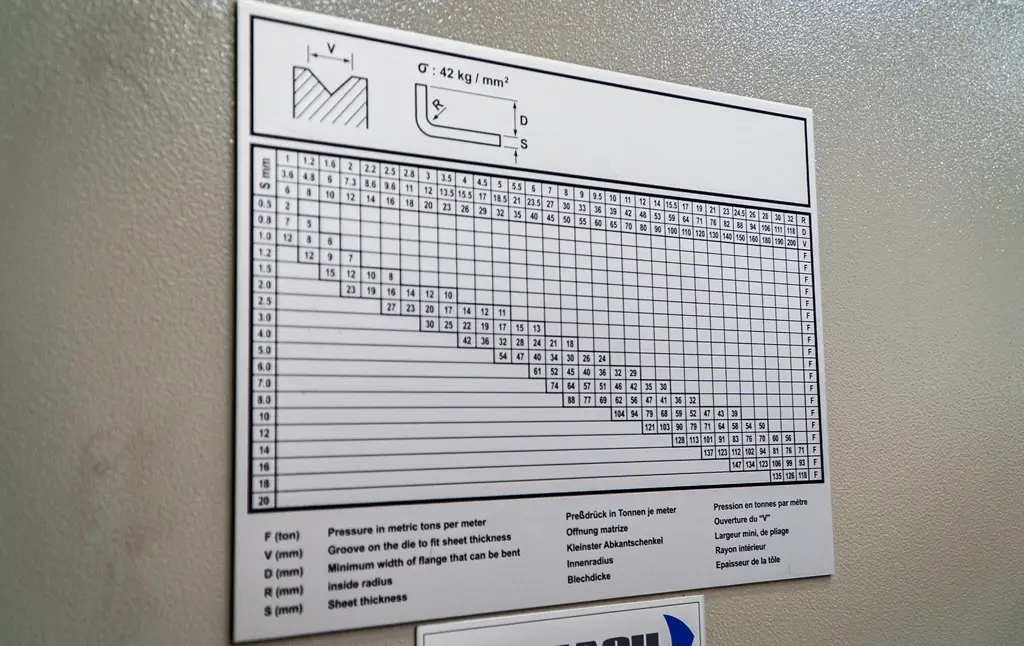
Material thickness and bend length are the starting point for press brake selection, but they do not establish capacity on their own. Material strength, forming method and tooling determine the.. Read More
Comments Off on Choosing a press brake controller and offline programming package
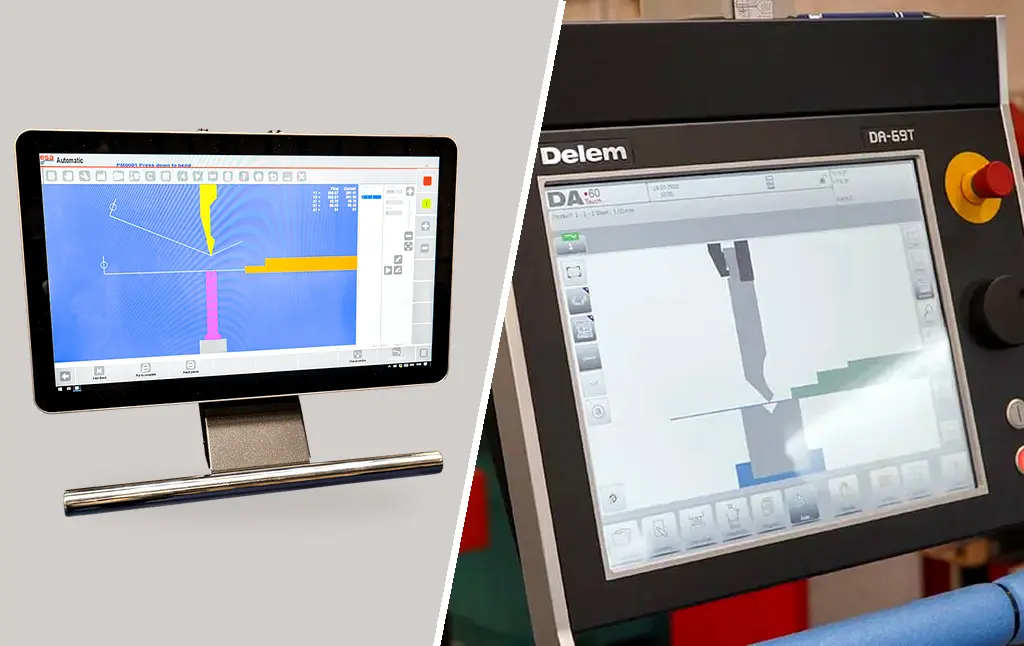
A controller should help your team turn approved drawings into repeatable bending jobs. A large screen or an extensive list of software features is useful only when the quoted package.. Read More
Comments Off on Choosing a CNC press brake backgauge for complex components
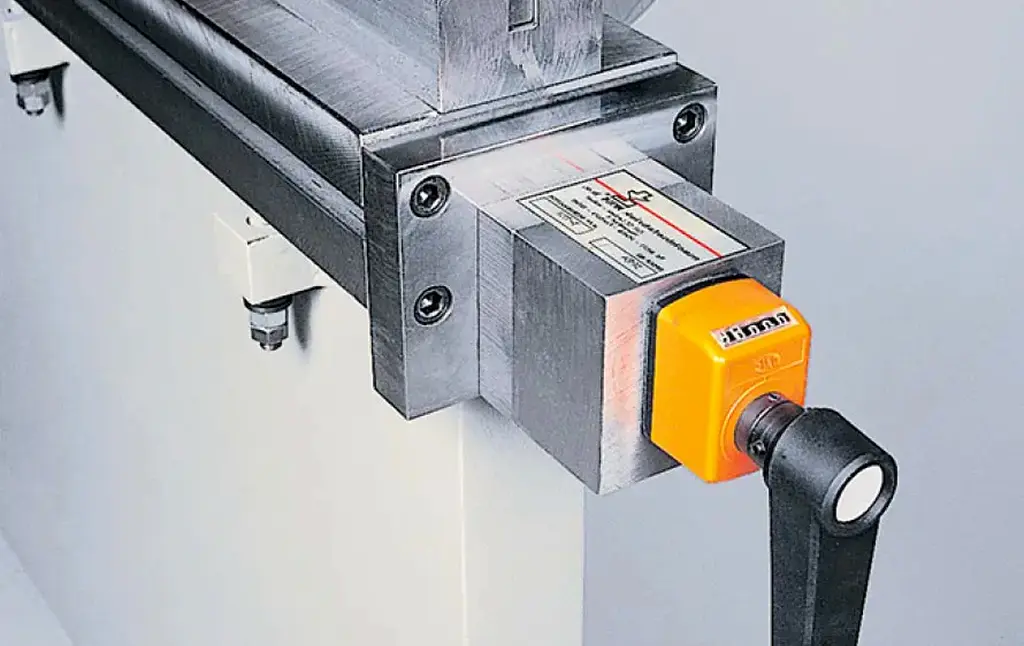
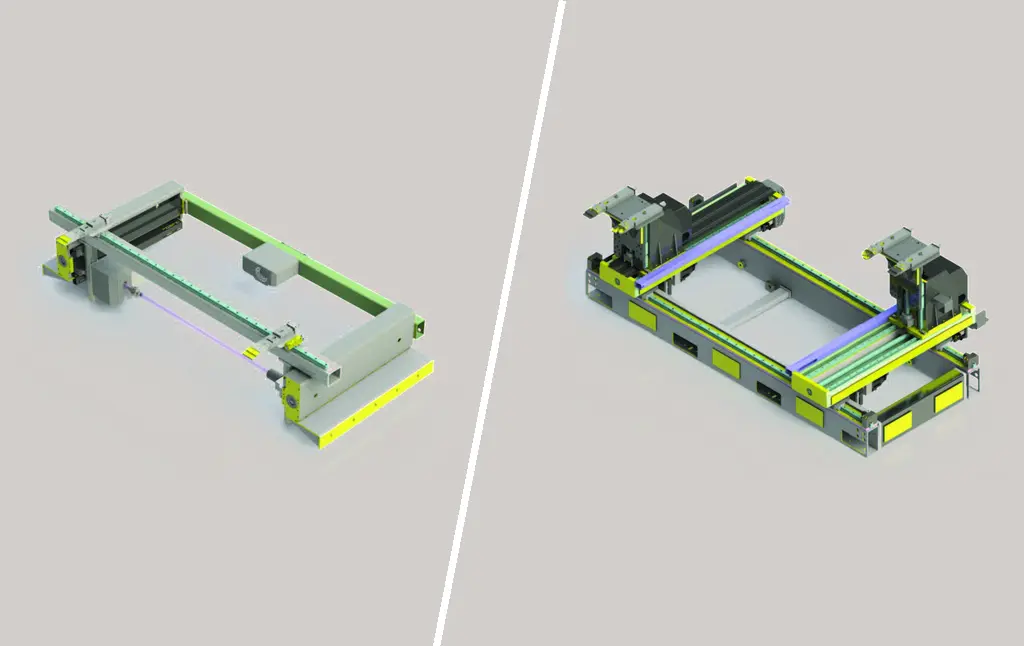
The backgauge provides a repeatable reference for positioning a component before a bend. Choosing it well means checking the reference available at every stage of forming, not simply ordering the.. Read More
Comments Off on Press brake axes explained: choosing the movements your components need
A press brake advertised as four, six or eight axis does not tell you everything you need to know about its capability. Suppliers may count ram movements, backgauge movements and.. Read More
Comments Off on From Fibre Laser to Press Brake Removing the Next Production Bottleneck
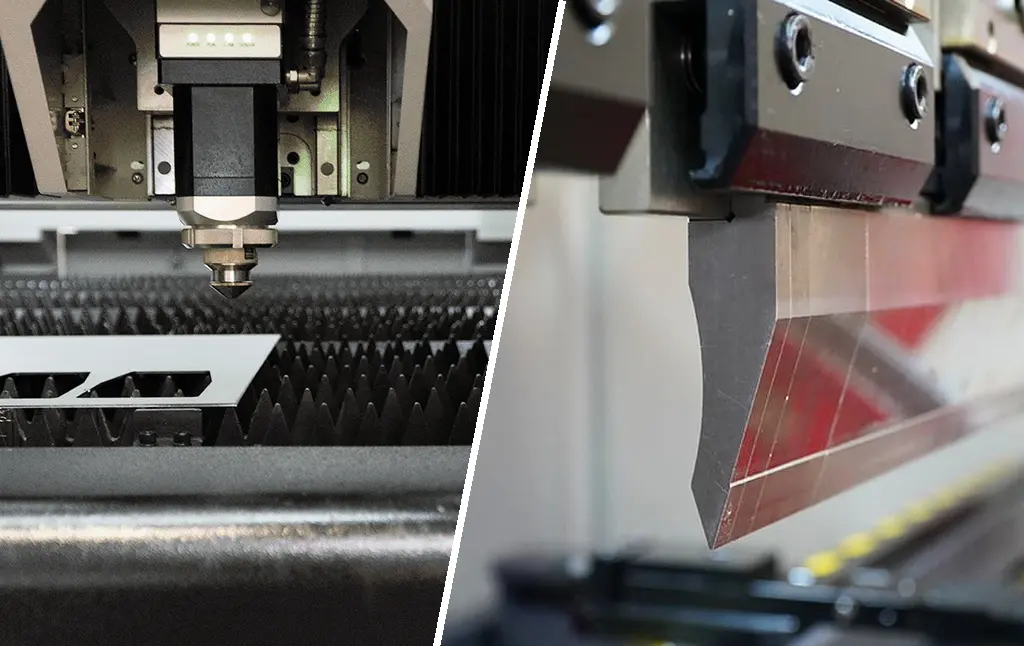
Increasing fibre laser output can reveal a problem elsewhere in the workshop: components reach bending faster than the press brake team can process them. The result is more work in.. Read More
Comments Off on Designing Fibre Laser Nests for Automated Production
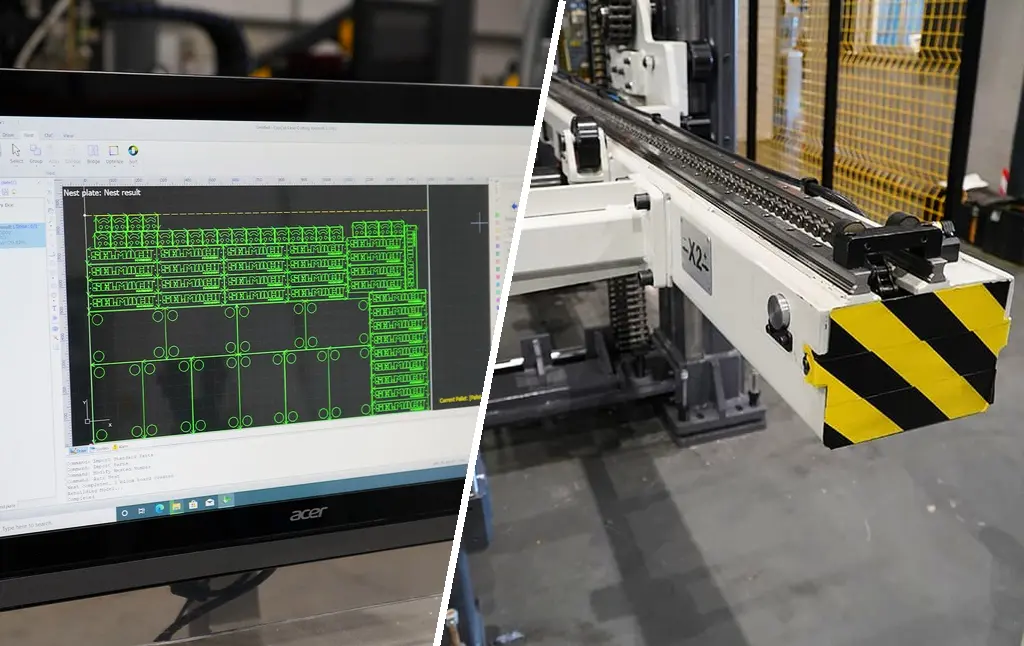
A good fibre laser nest uses material efficiently. An automation-ready nest also allows parts and skeletons to move through the intended handling process reliably... Read More
Comments Off on Planning a Fibre Laser Automation Layout
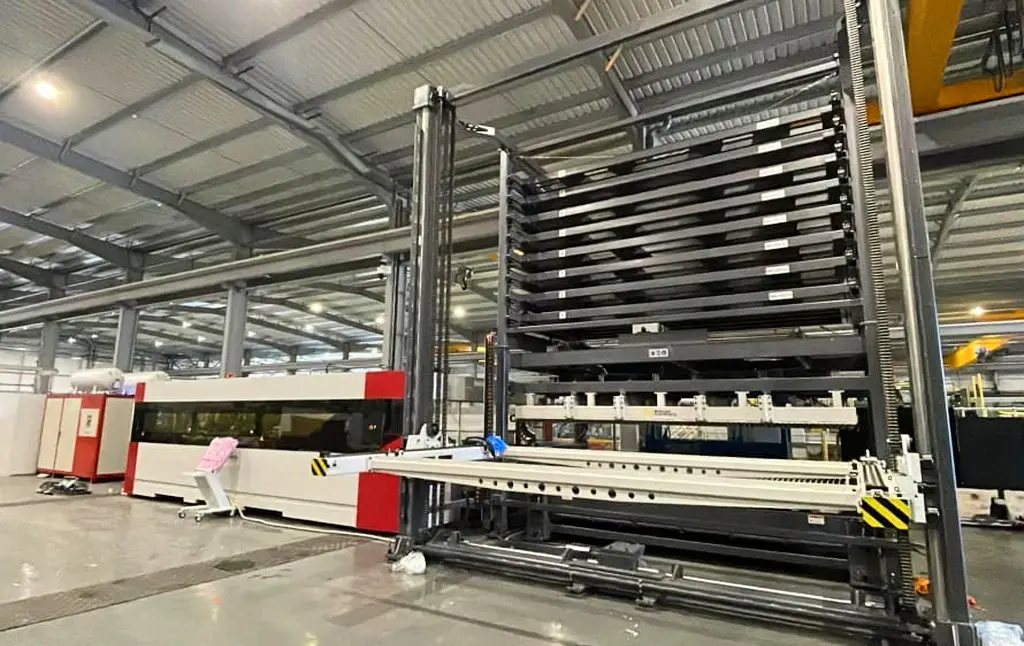
The footprint of a fibre laser and its automation equipment is only part of the space required. A workable layout also needs routes for stock, finished parts, scrap, operators and.. Read More
Comments Off on Can Automation Be Added to an Existing Fibre Laser
Adding automation to an existing fibre laser may be possible, but compatibility needs to be assessed for the specific machine and proposed handling equipment. A system designed for one configuration.. Read More
Comments Off on How to Measure Fibre Laser Productivity
A fast cutting demonstration does not tell you how much useful work a fibre laser will deliver in a normal week. Production includes loading, programme preparation, job changes, handling and.. Read More
Comments Off on Tube Laser Unloading and Finished Part Collection Explained
Tube laser automation is often discussed in terms of loading raw stock. The other end of the machine deserves equal attention: how finished components leave the cutting area and reach.. Read More
Comments Off on Tube Laser Cutting for Faster Welding and Assembly
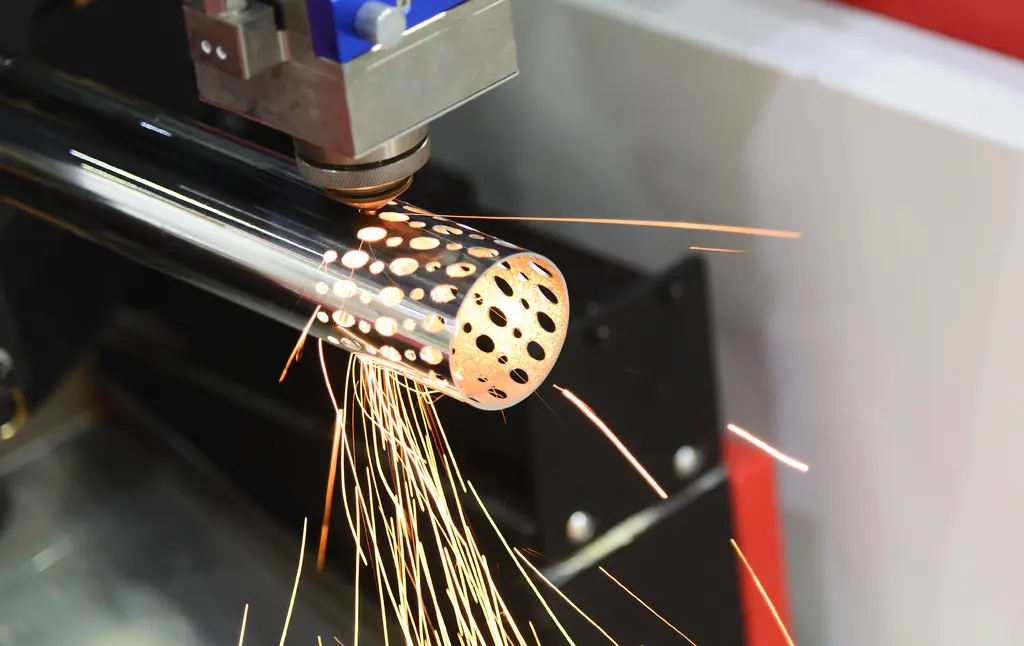
Tube laser cutting can combine several preparation operations in one programmed process. Its wider value often appears at the welding bench, where accurately positioned features can reduce marking out and.. Read More