
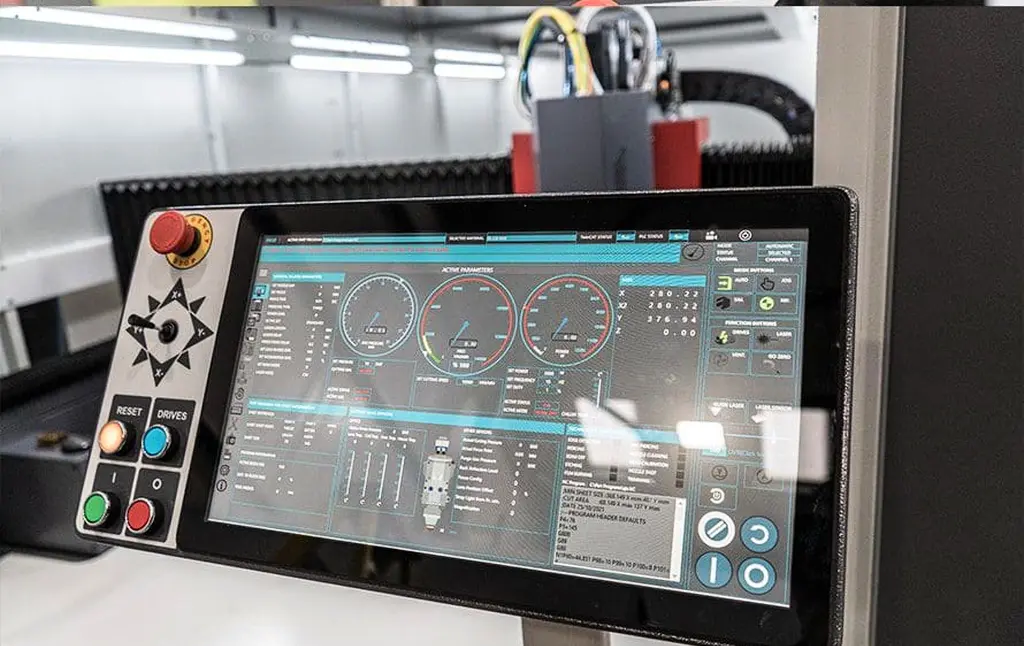
A fast cutting demonstration does not tell you how much useful work a fibre laser will deliver in a normal week. Production includes loading, programme preparation, job changes, handling and the occasional interruption.
The most useful measures show accepted work completed within the time available. They should also reveal why output falls short, so that the next improvement addresses the right problem.
Define the output you want to improve
For a repeat component, accepted parts per planned production hour can be useful. For mixed fabrication work, raw part counts can mislead: a small bracket and a large complex panel are different workloads.
Choose a measure that reflects your production. This might be completed orders, accepted sheets of a defined job mix or standard hours of work completed. Keep the workload description alongside the result.
Avoid comparing two machines using different material thicknesses, geometries or acceptance requirements. A credible comparison needs equivalent work and a consistent definition of completion.
Record planned time consistently
Decide what counts as planned production time before collecting figures. Make clear how breaks, scheduled maintenance and periods with no work released will be treated.
Then distinguish cutting time from other activity. Loading, unloading and programme changes may be necessary productive tasks, but they are not the same as the laser cutting material.
If you change the time definition between weeks, an apparent improvement may be a reporting change. Use the same definitions and explain any exceptions in the record.
Give interruptions useful categories
Record the main reason whenever the intended production cycle stops. Practical categories include material unavailable, programme not ready, loading or collection delay, consumable attention, equipment fault and downstream congestion.
Keep categories simple enough for the team to use consistently. A large number of highly specific codes can be less useful than a small set that identifies the dominant causes.
Where activities overlap, avoid counting the same lost minutes twice. If the machine is waiting for both material and a programme, use an agreed method to record the primary cause or split the interval consistently.
Count accepted output
Parts that need rework or replacement consume capacity without completing the order. Record accepted quantities and the reasons for rejected work.
An illustrative shift might produce 100 components, of which 95 meet the agreed acceptance requirements. Its first-pass acceptance rate is 95%. That figure says nothing about cutting speed on its own, but highlights a quality loss that a total part count would hide.
For mixed work, record quality by job or part family so that difficult components do not disappear inside a workshop-wide average.
Use OEE with reliable inputs
Overall equipment effectiveness combines availability, performance and quality. Availability compares operating time with planned production time. Performance compares actual output with a validated production standard. Quality describes the accepted share of output.
The performance input is often difficult for mixed laser work. A standard must represent the actual job and clearly state which activities it includes. Without that basis, a single OEE percentage can create false confidence.
You do not need a complex dashboard to begin. A consistent record of accepted output, planned time and the main interruptions can already identify useful improvements.
Check where the output goes next
A laser can appear more productive while the workshop completes no additional orders. This happens when extra cut parts accumulate before deburring, bending or welding.
Measure the queue after cutting and the time taken for complete jobs to reach the next operation. Selmach’s batch size and automation guide provides useful background for reviewing the whole route.
Include handling effort when assessing automation. Fewer interruptions and less manual sorting may be more valuable than a small change in cutting speed.
Turn figures into a practical improvement
Collect a representative baseline, identify the largest recurring loss and change one part of the process. Then compare results using a similar workload and the same definitions.
Selmach can help you review fibre laser equipment and handling options against your production record. Bring examples of the work and the delays you want to remove, alongside the output target.
Published 13th October 2026