
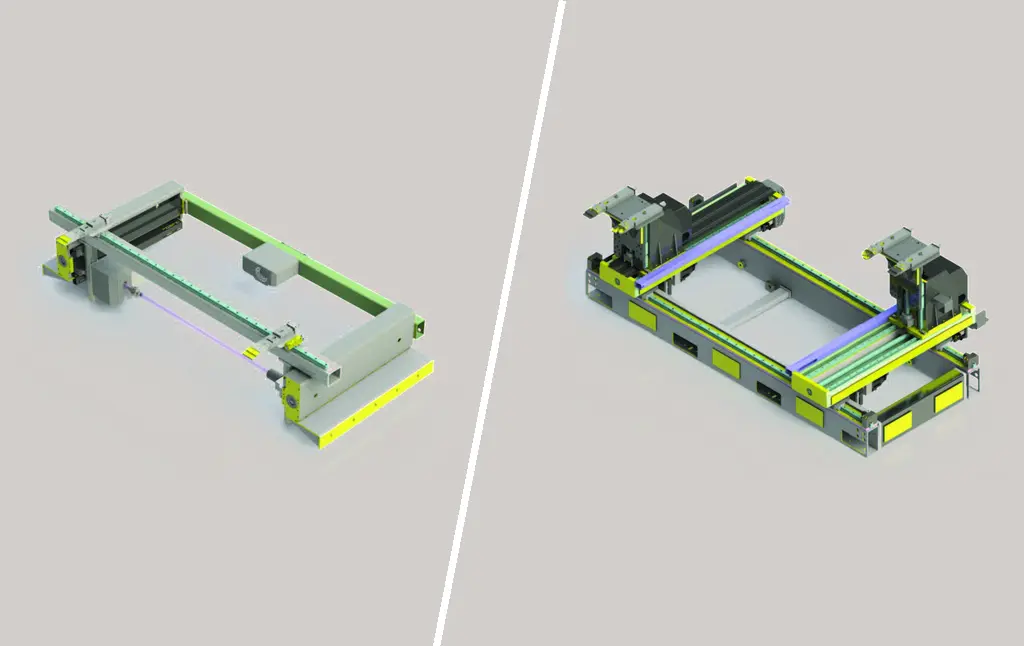
A press brake advertised as four, six or eight axis does not tell you everything you need to know about its capability. Suppliers may count ram movements, backgauge movements and crowning differently. Ask for a list of the controlled movements and select them around the parts you make.
Ram axes and backgauge axes are different
Y1 and Y2 describe independent control of the two sides of the ram on a synchronised hydraulic press brake. X describes backgauge depth: movement towards or away from the bending line. R describes backgauge height. Z1 and Z2 describe the lateral positions of the gauge fingers along the working length.
Where fitted, independent X1/X2 or R1/R2 movements allow the fingers to occupy different depth or height positions. Naming conventions vary, so confirm the actual mechanical arrangement. A controller capable of managing extra axes does not mean those movements are fitted to the machine.
What extra movements change
Programmable height can help gauge a component at different stages of a multi-bend sequence. Programmable lateral positioning can reduce manual finger adjustments between jobs. Independent depth positioning can be useful for some angled or asymmetric gauging arrangements. Each movement should solve a requirement shown on your drawings.
A six-axis package might describe Y1, Y2, X, R, Z1 and Z2: two ram axes and four backgauge axes. It would be misleading to call that a six-axis backgauge. CNC crowning may be listed separately or included in a supplier’s total.
Choose from the component, not the number
For straightforward brackets using the same gauge references, a simpler configuration may be sufficient. For a mixture of boxes, channels and asymmetric components, assess finger access, repositioning and support through the complete bend sequence. More movements cannot compensate for unsuitable tooling or insufficient clearance.
Compare the same drawing on each proposed configuration. Record manual adjustments, regrips, setup time and accepted component dimensions. Confirm how the operator recalls finger positions and whether the fingers can reach the required reference without contacting a formed flange.
Specify a PBXS configuration clearly
The Morgan Rushworth PBXS is Selmach’s premium CNC hydraulic press brake range. It has four CNC-controlled axes as standard: Y1 and Y2 for the ram, X for backgauge depth and R for backgauge height. Lateral finger positioning is manual as standard, with optional CNC movements available for more demanding components. Ask Selmach to specify the ram axes, backgauge movements, crowning, controller and tooling as separate items. The quotation should identify standard equipment and selected options for the particular model.
Send your material grades, thicknesses, maximum bend lengths and representative drawings. Include awkward returns or unequal flanges rather than only your easiest part. Selmach can assess which configuration deserves a demonstration and quotation.
Questions to include in your enquiry
Which movements are CNC-controlled, and which are manually adjusted? Does the axis count include crowning? What are the actual finger travel and load limits? Can the proposed configuration complete our bend sequence? Which software functions and accessories are included?
Use our backgauge selection guide for the mechanical details and our tooling guide for clearance considerations. Review the PBXS range with these requirements together before selecting a model.
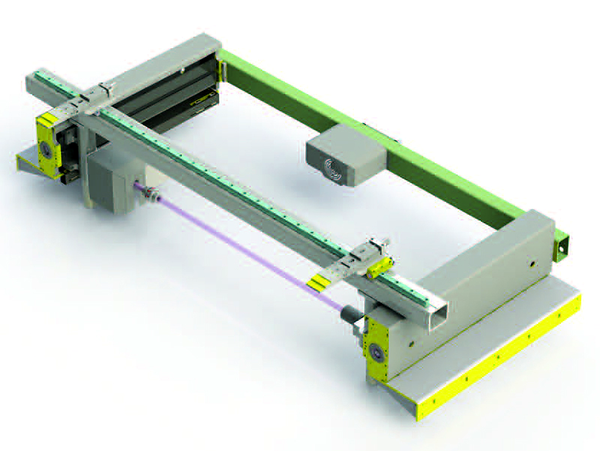
2 Axis – X and R
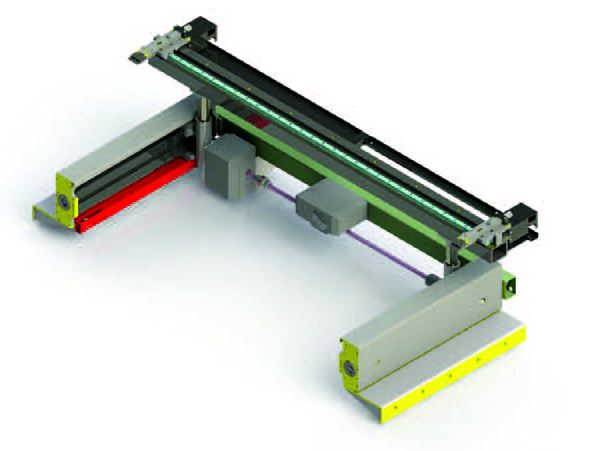
4 Axis – X, R, Z1, Z2
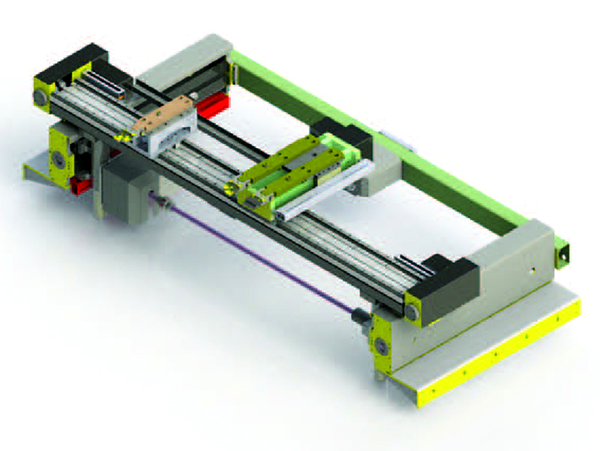
5 Axis – X, R, X5, Z1, Z2
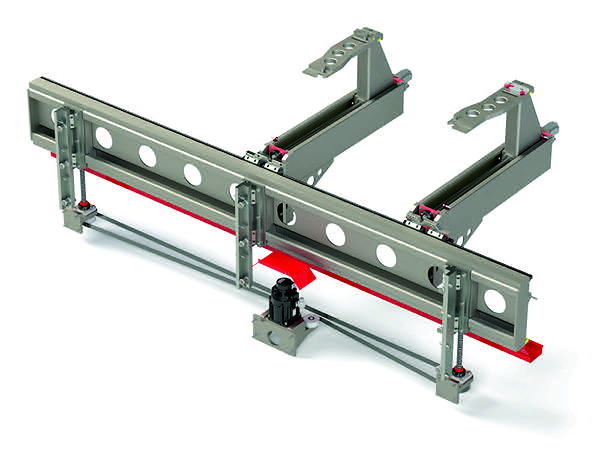
5 Axis – X1, X2, R, Z1, Z2
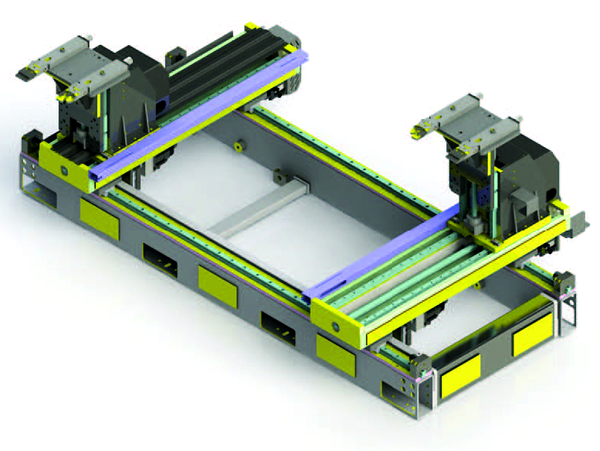
6 Axis – X1, R1, Z1, X2, R2, Z2
Published 21st October 2026